
Featured CE-Certified Medical Furniture & Mobility Range
Rigorous clinical-grade manufacturing designed for acute care facilities, rehabilitation centers, and international B2B distributors.
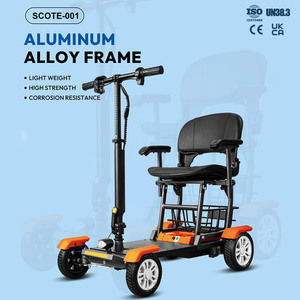
Lightweight Disability Mobility Scooter Electric Wheelchair
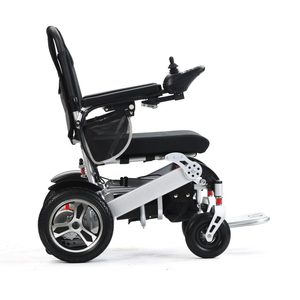
Wholesale Lithium Battery Motorized Foldable Wheelchair
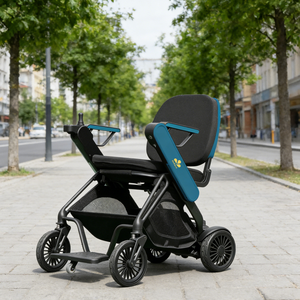
ZW505 Intelligent Folding Electric Wheelchair with APP
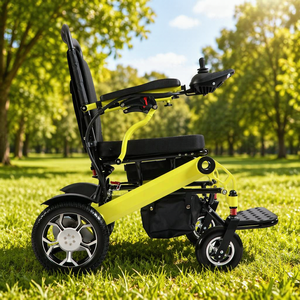
Portable Folding Power Wheelchair & Mobility Scooter
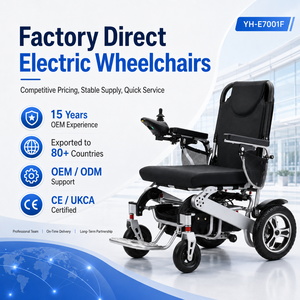
Custom Color Aluminum Alloy Smart Reclining Wheelchair
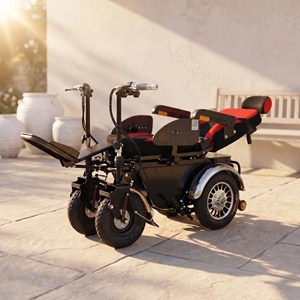
Motor Driven Standing Wheelchair with Lifting Legrest
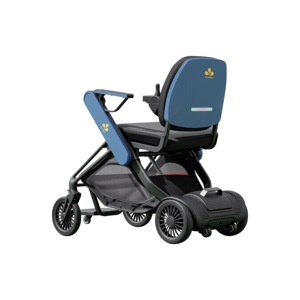
ZW505 All-Terrain Auto-Folding Power Wheelchair
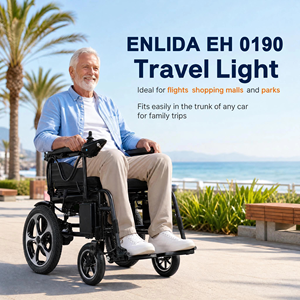
ENLIDA EH0190 Heavy Duty Folding Electric Wheelchair
Executive Summary: Navigating Modern Overbed Table Procurement & Manufacturing Excellence
In modern hospital administration and long-term care management, the overbed table serves as a critical, multi-functional focal point of patient-centric care. Far beyond simple surface utility, contemporary medical overbed tables represent sophisticated engineering solutions designed to satisfy stringent hygiene parameters, ergonomic accessibility, structural durability, and seamless integration with electric medical beds. As global healthcare infrastructure expands, procurement directors, hospital supply chain executives, and medical device distributors face mounting pressure to source CE-certified equipment that strictly adheres to European Medical Device Regulation (EU MDR 2017/745) and international quality frameworks.
This industry white paper, authored by senior medical equipment manufacturing strategists at Anrace Assistive Mobility, analyzes the technical benchmarks, material engineering standards, OEM manufacturing workflows, and regulatory compliance protocols that define world-class overbed table production. By offering deep technical insights and empirical evaluation metrics, we aim to provide global buyers with actionable information gain to make informed, risk-averse procurement decisions.
Core Procurement Insight: CE compliance for medical overbed tables is not merely a label—it requires rigorous structural fatigue testing, bio-compatibility verification of surface laminates (ISO 10993), chemical resistance against hospital-grade disinfectants, and strict anti-entrapment geometry compliant with ISO 60601-2-52 patient safety norms.
1. Engineering Standards & Structural Architecture of CE Certified Overbed Tables
An exemplary overbed table must balance high load-bearing structural integrity with smooth, low-effort vertical adjustability. Modern manufacturing factories utilize three primary structural architectures:
A. Gas-Spring Pneumatic Counterbalance Systems
Pneumatic overbed tables leverage precision-calibrated internal gas struts that enable effortless one-handed height adjustment. By pressing a single release lever, the patient or caregiver can smoothly elevate or lower the tabletop between 700 mm and 1050 mm. The primary advantage of high-grade gas-strut mechanisms lies in their fail-safe upward displacement: if a patient's legs or electric bed frame rises beneath the table, the mechanism yields upward automatically, preventing crushing injuries or structural failure.
B. Hydraulic Auto-Locking Telescopic Columns
Designed for heavy-duty hospital environments, hydraulic systems utilize sealed fluid chambers to deliver exceptional static weight capacity—frequently supporting upward of 45 kg to 60 kg without deflection. Precision extruded aluminum or cold-rolled steel column profiles are hard-anodized or powder-coated to eliminate metal-on-metal friction and prevent corrosion from frequent washdowns.
C. Low-Profile C-Shaped Base Dynamics
The base structural geometry dictates physical compatibility with clinical furniture. Premium factories design low-clearance C-frame bases with profile heights under 90 mm (fitted with ultra-low clearance swivel casters). This allows the table base to slide effortlessly beneath low-height ICU beds, patient lift chairs, and powered wheelchairs, ensuring zero spatial obstruction during patient transfer procedures.
| Technical Feature | Standard Commercial Grade | Clinical-Grade CE Certified (Anrace Spec) | Clinical Benefit |
|---|---|---|---|
| Base Frame Material | Standard Q235 Mild Steel | Heavy-Gauge Cold-Rolled Carbon Steel / Extruded Aluminum | Superior structural rigidity, zero sagging under load. |
| Surface Top Coating | Standard PVC Foil Wrap / MDF | Thermoformed ABS Molded / High-Pressure Compact Laminate (HPL) | 100% waterproof, seamless fluid retention rim, anti-microbial. |
| Height Lift Mechanism | Manual Screw Lock / Basic Spring | Enclosed Gas-Strut Pneumatic Auto-Rise System | Single-touch height adjustment with anti-crush safety stop. |
| Disinfectant Resistance | Degrades with Alcohol Exposure | Resistant to Bleach, Quaternary Ammonium & 70% Isopropyl | Prevents cracking, yellowing, or chemical peeling over time. |
| Caster Specification | 2-inch Plastic Single Casters | 2-inch Medical Swivel Twin-Wheel Casters with Non-Marking TPU | Silent maneuverability, non-marking, twin-locking brakes. |
2. Infection Control & Advanced Surface Material Science
In post-pandemic healthcare architecture, nosocomial infection prevention (HAIs) is paramount. Hospital overbed tables are among the most frequently touched surfaces in patient isolation rooms, making material selection a direct variable in patient safety.
- Seamless Blow-Molded ABS Tops: Manufactured using high-density Acrylonitrile Butadiene Styrene (ABS), these tabletops feature raised spill-retaining perimeters that capture up to 500 ml of spilled liquid. The non-porous surface eliminates seams where bacteria, staphylococcus, or viral pathogens can hide.
- High-Pressure Laminate (HPL) Phenolic Resin: Ideal for surgical suites and burn units, HPL tops offer extreme thermal resistance, impact resistance, and imperviousness to aggressive chemical agents used in terminal cleaning cycles.
- Silver-Ion Anti-Microbial Additives: Leading factories integrate silver-ion compounding directly into the polymer matrix during molding. This provides continuous 24/7 antibacterial activity, reducing microbial bioburden by 99.9% over a 24-hour cycle.
3. Enterprise Advantages of Partnering with Anrace Manufacturing Infrastructure
As a leading global exporter of medical equipment and assistive mobility devices, Anrace Assistive Mobility Private Limited operates advanced, highly integrated manufacturing facilities located in HSIIDC IMT Rohtak, supported by strategic corporate operations in New Delhi, India. Our export operations serve healthcare retailers, OEM brands, and institutional buying syndicates across over 30 countries.
ISO 13485:2016 Certification
Full compliance with global medical device quality management systems, ensuring traceability from raw steel sourcing to final box sealing.
OEM & Custom Engineering
Bespoke color options, custom top dimensions, tablet/cup holder integrations, and private-label logo laser engraving for international distributors.
Optimized Bulk Shipping
Flat-pack knock-down (KD) packaging design maximizing 40ft HQ container loading capacity, significantly lowering landed logistics costs.
4. Future Procurement & Market Trends (2026–2030)
As healthcare systems shift toward digital patient monitoring and home hospital setups, the overbed table category is undergoing rapid evolutionary shifts:
- Smart IoT & Power Integration: Modern hospital buyers increasingly demand overbed tables equipped with embedded USB-C charging hubs, wireless smartphone charging pads, and strain-relief cable routing channels to support patient tele-health tablets and personal electronic devices.
- Bariatric-Rated Heavy-Load Capacity: With global patient demographics shifting, standard overbed tables with 15 kg weight ratings are being superseded by heavy-duty 45 kg+ bariatric units capable of supporting heavy clinical monitoring equipment, meal trays, and emergency upper-body leaning.
- Multi-Functional Rehabilitation Convergence: Hospital buyers prefer versatile equipment that bridges post-operative patient care with physical therapy—integrating tiltable reader tops, pull-out vanity mirrors, and height adjustments compatible with both ICU beds and specialized motorized power wheelchairs.
Frequently Asked Questions (FAQ) for B2B Procurement
Technical clarity and regulatory compliance answers for hospital purchasing agents, medical supply importers, and distributor partners.
Partner with a Trusted CE Certified Manufacturer
Elevate your product portfolio with world-class medical furniture, overbed tables, and assistive mobility equipment. Contact our technical export sales team today for factory-direct wholesale pricing, technical specifications, and sample evaluation kits.